Diamond dish wheels and cup wheels
Geometry:4A2


D(mm)
|
W(mm)
|
X(mm)
|
T(mm)
|
E(mm)
|
J(mm)
|
H(mm)
|
75
|
5
|
2-3-4-5
|
E+X
|
6
|
38
|
Must be
specified on order |
10
|
2-3-4-5
|
E+X
|
6
|
38
| ||
100
|
4
|
2-3-4-5
|
E+X
|
6
|
63
| |
5
|
2-3-4-5
|
E+X
|
6
|
63
| ||
6
|
2-3-4-5
|
E+X
|
6
|
63
| ||
10
|
2-3-4-5
|
E+X
|
6
|
63
| ||
125
|
4
|
2-3-4-5
|
E+X
|
7
|
80
| |
5
|
2-3-4-5
|
E+X
|
7
|
80
| ||
6
|
2-3-4-5
|
E+X
|
7
|
80
| ||
10
|
2-3-4-5
|
E+X
|
7
|
80
| ||
150
|
4
|
2-3-4-5
|
E+X
|
9
|
90
| |
5
|
2-3-4-5
|
E+X
|
9
|
90
| ||
6
|
2-3-4-5
|
E+X
|
9
|
90
| ||
10
|
2-3-4-5
|
E+X
|
9
|
90
| ||
200
|
10
|
2-3-4-5
|
E+X
|
10
|
133
|
Geometry:4B1

D(mm)
|
W(mm)
|
T(mm)
|
H(mm)
|
50
|
3
|
5
|
Must be specified on order
|
75
|
5
|
8
| |
80
|
5
|
8
| |
100
|
5
|
10
| |
8
|
10
| ||
125
|
8
|
10
| |
12
|
12
| ||
150
|
8
|
10
| |
12
|
12
|
Geometry:6A2

D(mm)
|
W(mm)
|
X(mm)
|
T(mm)
|
A(mm)
|
E(mm)
|
H(mm)
|
50
|
7
|
2-3-4-5
|
A+X
|
17
|
6
|
Must be
specified on order |
75
|
5
|
2-3-4-5
|
A+X
|
19
|
10
| |
10
|
2-3-4-5
|
A+X
|
19
|
10
| ||
100
|
5
|
2-3-4-5
|
A+X
|
27
|
10
| |
10
|
2-3-4-5
|
A+X
|
27
|
10
| ||
125
|
5
|
2-3-4-5
|
A+X
|
29
|
10
| |
10
|
2-3-4-5
|
A+X
|
29
|
10
| ||
15
|
2-3-4-5
|
A+X
|
29
|
10
| ||
20
|
2-3-4-5
|
A+X
|
29
|
10
| ||
150
|
5
|
2-3-4-5
|
A+X
|
29
|
10
| |
10
|
2-3-4-5
|
A+X
|
29
|
10
| ||
20
|
2-3-4-5
|
A+X
|
29
|
10
| ||
175
|
25
|
2-3-4-5
|
A+X
|
25
|
13
| |
200
|
20
|
2-3-4-5
|
A+X
|
37
|
13
|
Geometry:9A3

D(mm)
|
W(mm)
|
X(mm)
|
T(mm)
|
A(mm)
|
E(mm)
|
H(mm)
|
150
|
6
|
2-3-4-5
|
A+2X
|
14
|
12
|
Must be
specified on order |
175
|
6
|
2-3-4-5
|
A+2X
|
14
|
12
| |
200
|
6
|
2-3-4-5
|
A+2X
|
14
|
12
|
Geometry:11A2

D(mm)
|
W(mm)
|
X(mm)
|
T(mm)
|
A(mm)
|
E(mm)
|
J(mm)
|
H(mm)
|
75
|
4
|
2-3-4-5
|
A+X
|
20
|
10
|
61
|
Must be
specified on order |
5
|
2-3-4-5
|
A+X
|
20
|
10
|
61
| ||
6
|
2-3-4-5
|
A+X
|
20
|
10
|
61
| ||
100
|
5
|
2-3-4-5
|
A+X
|
33
|
10
|
77
| |
10
|
2-3-4-5
|
A+X
|
33
|
10
|
77
| ||
15
|
2-3-4-5
|
A+X
|
33
|
10
|
77
| ||
125
|
5
|
2-3-4-5
|
A+X
|
33
|
10
|
102
| |
10
|
2-3-4-5
|
A+X
|
33
|
10
|
102
| ||
15
|
2-3-4-5
|
A+X
|
33
|
10
|
102
| ||
150
|
10
|
2-3-4-5
|
A+X
|
33
|
10
|
127
| |
20
|
2-3-4-5
|
A+X
|
33
|
10
|
127
|
Geometry: 11V9

D(mm)
|
X(mm)
|
W(mm)
|
T(mm)
|
E(mm)
|
H(mm)
|
75
|
1.5
|
8--10
|
30
|
10
|
Must be specified on order
|
100
|
3
|
7--10
|
40
|
10
| |
125
|
3
|
7--10
|
45
|
10
| |
150
|
5
|
7--10
|
45
|
10
|
Geometry:12A2 20


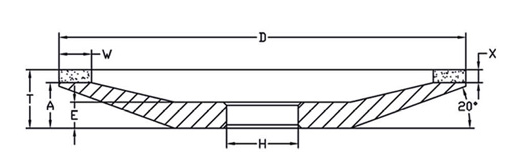
D(mm)
|
W(mm)
|
X(mm)
|
T(mm)
|
A(mm)
|
E(mm)
|
H(mm)
|
50
|
2
|
2--3
|
A+X
|
8
|
6
|
Must be
specified on order |
3
|
2-3-4-5
|
A+X
|
8
|
6
| ||
4
|
2-3-4-5
|
A+X
|
8
|
6
| ||
75
|
5
|
2-3-4-5
|
A+X
|
9
|
6
| |
10
|
2-3-4-5
|
A+X
|
9
|
6
| ||
100
|
5
|
2-3-4-5
|
A+X
|
10
|
8
| |
10
|
2-3-4-5
|
A+X
|
10
|
8
| ||
125
|
5
|
2-3-4-5
|
A+X
|
10
|
8
| |
10
|
2-3-4-5
|
A+X
|
10
|
8
| ||
150
|
5
|
2-3-4-5
|
A+X
|
13
|
9
| |
6
|
2-3-4-5
|
A+X
|
13
|
9
| ||
10
|
2-3-4-5
|
A+X
|
13
|
9
| ||
15
|
2-3-4-5
|
A+X
|
13
|
9
| ||
200
|
10
|
2-3-4-5
|
A+X
|
13
|
10
| |
20
|
2-3-4-5
|
A+X
|
13
|
10
|
Geometry:12A2

D(mm)
|
W(mm)
|
X(mm)
|
T(mm)
|
A(mm)
|
E(mm)
|
H(mm)
|
50
|
3
|
2-3--4
|
A+X
|
17
|
6
|
Must be
specified on order |
4
|
2-3--4
|
A+X
|
17
|
6
| ||
75
|
5
|
2-3-4-5
|
A+X
|
22
|
9
| |
6
|
2-3-4-5
|
A+X
|
22
|
9
| ||
10
|
2-3-4-5
|
A+X
|
22
|
9
| ||
100
|
3
|
2-3-4-5
|
A+X
|
29
|
10
| |
5
|
2-3-4-5
|
A+X
|
29
|
10
| ||
10
|
2-3-4-5
|
A+X
|
29
|
10
| ||
125
|
4
|
2-3-4-5
|
A+X
|
29
|
10
| |
5
|
2-3-4-5
|
A+X
|
29
|
10
| ||
6
|
2-3-4-5
|
A+X
|
29
|
10
| ||
10
|
2-3-4-5
|
A+X
|
29
|
10
| ||
15
|
2-3-4-5
|
A+X
|
29
|
10
| ||
150
|
5
|
2-3-4-5
|
A+X
|
29
|
10
| |
6
|
2-3-4-5
|
A+X
|
29
|
10
| ||
10
|
2-3-4-5
|
A+X
|
29
|
10
| ||
15
|
2-3-4-5
|
A+X
|
29
|
10
| ||
200
|
10
|
2-3-4-5
|
A+X
|
37
|
12
| |
20
|
2-3-4-5
|
A+X
|
37
|
12
|
Geometry:12V2


D(mm)
|
W(mm)
|
X(mm)
|
T(mm)
|
H(mm)
|
50
|
2
|
2
|
10
|
Must be specified on order.
|
75
|
3
|
3
|
13
| |
5
|
3
|
13
| ||
10
|
3
|
13
| ||
100
|
3
|
3
|
13
| |
5
|
3
|
13
| ||
10
|
3
|
13
| ||
125
|
4
|
3--5
|
16
| |
5
|
3
|
16
| ||
10
|
3
|
16
| ||
150
|
5
|
3
|
16
| |
10
|
3
|
16
|


